
Sustainable Synthetic Leather Roll & Cord Base Materials
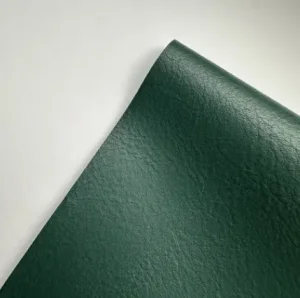
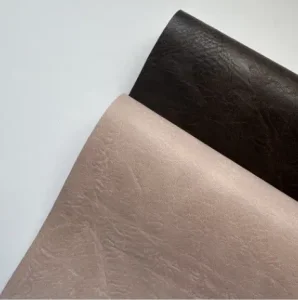
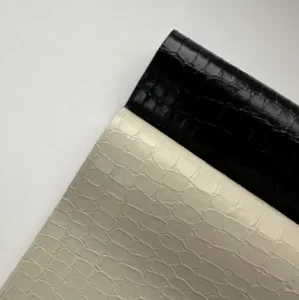
Explore our core engineered substrates and high-tensile synthetic leather materials formulated for custom cord cutting, continuous folding, braiding, and stitch-edge piping.
Global Enterprise Procurement Dynamics for Synthetic Leather Cords
In modern contract manufacturing, synthetic leather cordage has transformed from an ornamental trim into a critical structural component subjected to rigorous mechanical pull, constant skin contact, and aggressive chemical scrutiny.
Luxury Jewelry & Horology Trims
Global fashion houses and jewelry brands require micro-diameter cords (0.8mm to 2.5mm) exhibiting extreme colorfastness against human perspiration, zero phthalate leaching, and hypoallergenic biocompatibility. Cords must pass strict EN 1811 nickel-release contact testing and avoid toxic softening plasticizers.
- Sweat & sebum resistance: ISO 105-E04 Grade 4-5
- Braid uniformity: Strict ±0.05mm caliper tolerance
- Non-fraying micro-cores with thermal-seal capability
Footwear Lacing & Leather Goods
High-tier athletic lifestyle shoes, work boots, and luxury leather handbags demand round and flat synthetic leather cords engineered with reinforced internal high-tenacity polyester cores. This prevents mechanical necking, snapping under 450N+ dynamic eyelet tension, and abrasion during knot tying.
- Breaking strength: >500N per SATRA TM93 protocol
- Martindale abrasion: 50,000+ cycles dry/wet
- Knot-slip stability and consistent tensile modulus
Automotive Seating & Trim Piping
Tier-1 automotive interior suppliers integrate polyurethane welt cords and hollow piping profiles into seat covers, steering wraps, and door panels. These components must withstand continuous solar baking, VOC fogging limitations, and severe cold-crack resistance without hardening or embrittlement.
- DIN 75201 automotive fogging test: G > 90%
- Cold-crack threshold: -30°C per ISO 4646
- Flame retardancy conforming to FMVSS 302
Engineering Architecture: High-Yield Extrusion & Multi-Core Braiding
A comprehensive examination of how JiangXin New Material achieves industrial-grade dimensional accuracy, flexural fatigue resistance, and surface longevity in custom synthetic leather cords.
1. High-Density Microfiber Substrate
Our cord production starts from needle-punched sea-island microfiber nonwovens impregnated with bio-based or waterborne PU matrices. This replicates the collagen bundle network of genuine hide, providing natural stretch recovery and preventing hollow flattening during tight bends.
2. Laser-Guided Micro-Slitting
Continuous rotary cutting systems with ultrasonic stabilization slit parent rolls into ribbon widths down to 1.2mm with ±0.03mm precision. Laser-sealed edges eliminate loose micro-fibers, ensuring perfectly round profiles when routed into high-speed folding dies.
3. Zero-Solvent Polyurethane Skin
By eliminating DMF, toluene, and MEK through our 100% solvent-free casting lines, the resulting synthetic leather skin features dense aliphatic polymer networks. This achieves superior hydrolysis endurance, resisting 10-week Jungle Test degradation (70°C, 95% RH).
4. Composite Core Reinforcement
For demanding tensile loads, cords can be hollow-wound or wrapped over pre-stretched recycled PET monofilament or Kevlar aramids. This engineered core provides an unyielding breaking threshold while maintaining the soft, warm exterior haptics of luxury calfskin.
Technical Roadmap: Next-Generation Circular & Bio-Synthetics
Our R&D engineering roadmap maps the transition from conventional petrochemical PU cords to fully circular, bio-synthesized, and closed-loop performance trims.
Recycled Content Scaling
Achieving 30%–70% GRS/RCS certified recycled post-consumer polyester (rPET) in nonwoven backings and central core stabilizers. Complete transaction certificate traceability across all supply batches.
Agricultural Bio-Polyols
Replacing fossil petroleum-derived prepolymers with non-food agricultural waste polyols (corn stalks, sugarcane residue, castor oil). Bio-based carbon shares independently verified above 45% via ASTM D6866 radiocarbon analysis.
Waterborne Zero-Emission Cords
Complete phase-in of water-dispersed polyurethane (WPU) crosslinked with bio-based isocyanates. Zero VOC release during extrusion, zero wastewater discharge in cord finishing, and 100% skin-safe hypoallergenics.
Circular Closed-Loop Depolymerization
Development of mono-material PU cords capable of chemical recycling and closed-loop depolymerization into base monomers, establishing a cradle-to-cradle zero-landfill industrial lifecycle for trim components.
Material Benchmark: Synthetic Leather Cord vs. Alternative Substrates
A rigorous industrial comparison showing why multinational brands are replacing genuine leather cords and conventional PVC with engineered bio-based & RCS PU cords.
| Performance Metric | JiangXin Bio-Based / RCS PU Cord | Traditional Genuine Hide Cord | Commodity PVC Plastic Cord |
|---|---|---|---|
| Continuous Reel Length | Unlimited 500m–2000m continuous spool, 0 splices | Limited to 1.2m–1.8m hide cuts; requires glued joints | Continuous extrusion spooling |
| Caliper Uniformity | ±0.03 mm via laser-guided slitting & die folding | ±0.35 mm variation due to animal hide grain density | ±0.08 mm (tends to neck down under heat) |
| Environmental & Carbon Footprint | Low Scope 3 emissions; 4.68MW solar-powered campus | Severe carbon burden, deforestation, chromium tanning | Fossil dependent; high phthalate & chlorine content |
| Tensile Breaking Modulus | Engineered core yields up to >650 N | Unpredictable (150 N – 400 N) due to localized scar tissue | Moderate (200 N – 300 N), prone to plastic creep |
| Hydrolysis & Sweat Resistance | Grade 4-5 (Resists 10-week Jungle Test) | Poor; stiffens, cracks, and rots under sweat exposure | Good, but plasticizers leach out and harden surface |
| Chemical Compliance | REACH, RoHS, 6P-Free, OEKO-TEX, GRS/RCS Certified | Frequent chromium VI & formaldehyde contamination | Restricted under EU REACH Annex XVII & Prop 65 |
Localized Support & International Compliance Assurance
Our industrial engineering protocols guarantee rapid sampling turnarounds, verified chemical safety, and streamlined customs clearance across North American, European, and Asian supply chains.
Tier-1 Restricted Substance List (RSL)
Every cord lot is formulated to satisfy stringent international consumer safety standards, including EU REACH SVHC non-inclusion, California Proposition 65 total lead and phthalate limits, and OEKO-TEX Standard 100 Class I (safe for infant skin contact).
Rapid Prototype & Tooling Lab
Our in-house die shop allows rapid turnaround for custom cord profiles, flat ribbons, round stitch-fold piping, and multi-strand braided cordages. Lab swatches and custom color-match strike-offs are typically prepared within 3 to 5 working days.
Chain-of-Custody Transaction Certificates
Orders requesting RCS or GRS content are managed under strict chain-of-custody tracking. We furnish official Transaction Certificates (TCs) issued by accredited third-party auditing bodies (such as IDFL or Control Union) for seamless customs clearance.
Frequently Asked Questions: Synthetic Leather Cord Manufacturing
Direct technical guidance from our chemical formulation and production engineers regarding cord geometries, custom tooling, and quality assurance.
We manufacture continuous solid round cords (0.8mm to 10.0mm), flat strips/cords (1.5mm to 30.0mm width, 0.4mm to 2.5mm thickness), hollow tubing cords for jewelry, folded edge piping/welt cords with stitch margins for upholstery, and 3-strand to 16-strand hollow or core-filled braided cords.
Our cords utilize aqueous aliphatic polyurethane crosslinked topcoats cured at 135°C. This imparts dry and wet crock fastness of Grade 4.5+ per ISO 105-X12, completely preventing dye migration onto white canvas, apparel fabrics, or human skin even under high humidity.
Yes. We specialize in solvent-free polyurethane manufacturing where the resin is reacted directly without DMF (dimethylformamide), toluene, or MEK. This delivers an odorless, skin-safe cord with zero VOC emissions and exceptional flexural fatigue endurance.
Cords are precision-wound onto high-density flanged spools (50m, 100m, 200m, 500m, or continuous 1000m reels) equipped with anti-tangling tension flanges. This enables smooth feed into automated computerized sewing, shoe-lacing, or jewelry assembly machinery.
Yes. We offer continuous inline micro-embossing including classic nappa, milled grain, saffiano, suede/nubuck, or custom laser-engraved micro-geometric patterns. We can also integrate metallic foils, iridescent coatings, or reflective safety yarns into braided designs.
For standard catalog colors and dimensions, our trial MOQ starts at 500 meters per specification. For custom Pantone color matching, special core reinforcements, or proprietary embossed tooling, our baseline production run is typically 1,500 to 3,000 meters.
Engineered Synthetic Leather Substrates & Specialized References
Select from our high-performance circular and plant-origin synthetic leathers, engineered to meet stringent tensile, environmental, and flex-testing standards.
Accelerate Your Custom Cord Development Program
Partner directly with Yingde City JiangXin New Material Co., Ltd. (JX.ECO). Access our 135,733 m² clean-tech production campus, clean-chemistry PU formulations, and automated cord-folding and slitting facilities. Request customized engineering sample swatches, technical data sheets, and compliance packages today.